Explainer: Factory Audit Red Flags in Spinning Machinery
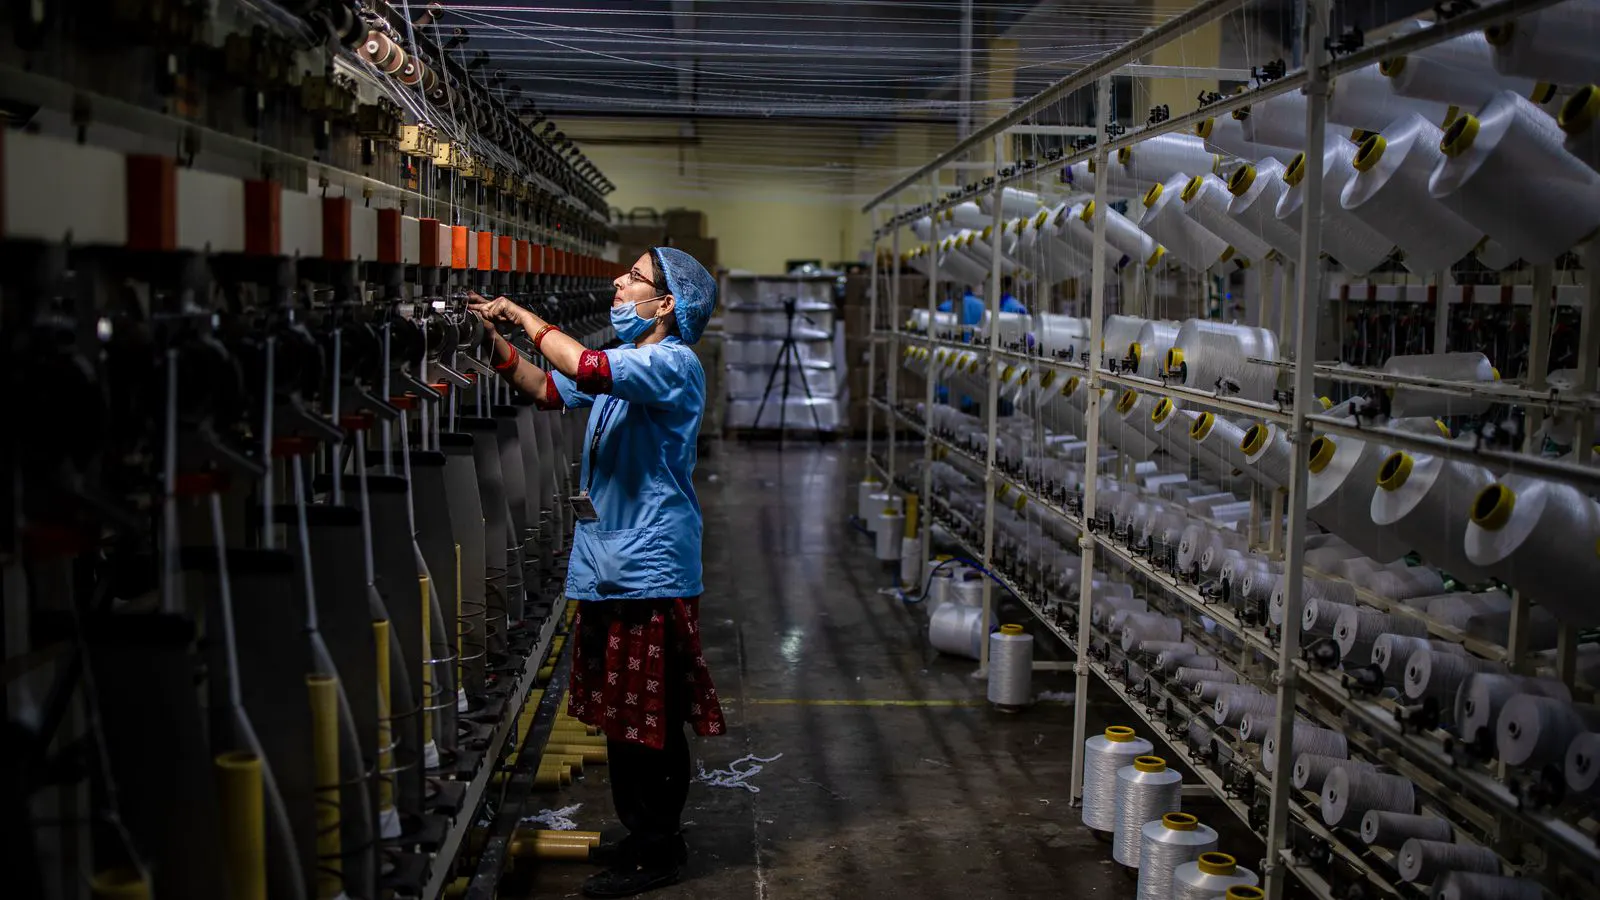
Factory audit red flags help procurement teams spot unreliable spinning machinery suppliers. This explainer defines key warning signs, shows how they affect sourcing, and gives a worked example of identifying gaps in supplier verification.
- Factory audit red flags include weak supplier verification, unclear production capacity, and missing spare parts documentation.
- Each flag affects sourcing decisions by changing risk, cost, and delivery reliability.
- A worked example shows how a missing production capacity check exposes a supplier's true limits.
- Auditors should use documents, observations, and direct questions to confirm supplier claims.
- Consistent checks during site visits reduce post-delivery disputes.
What a factory audit covers
A factory audit is a structured site visit to evaluate whether a spinning machinery supplier can deliver reliable equipment, parts, and support. It goes beyond a showroom tour. The auditor checks the factory floor, the workshop, the warehouse, and the paperwork. The goal is to confirm that the supplier’s stated capabilities match what is actually happening inside the plant.
Supplier verification is the process of confirming that a company is who it says it is. This includes checking legal status, production records, and the ability to meet technical requirements. In spinning machinery, this matters because machines are complex. A rotor, ring, or compacting machine is not a simple item. It depends on precision parts, calibration, and ongoing service.
The audit also includes a production capacity check. This means confirming whether the supplier can actually build, test, and ship the machines in the quantities the buyer needs. Many suppliers claim capacity without enough tooling, skilled labor, or testing space. The audit exposes these gaps.
Why red flags matter in sourcing
Red flags are warning signs that something is wrong. They are not always proof of fraud. Sometimes they indicate poor management, outdated processes, or unclear planning. But they do affect sourcing decisions.
If a supplier shows weak documentation, the buyer cannot trust future delivery dates. If the factory floor is disorganized, the risk of assembly errors rises. If spare parts are not stored properly, downtime after installation becomes more likely.
These signals matter because spinning machinery projects are long-term. The buyer is not just buying a machine. The buyer is entering a relationship with a supplier for maintenance, upgrades, and replacement parts. A bad start creates problems years later.
A worked example helps. A procurement manager visits a spinning machinery supplier for a potential order of ring spinning frames. During the audit, the manager sees the assembly area. The frames are partially built, but there is no visible testing station. The supplier says testing is done at a partner facility. The manager asks for the partner’s name and the testing report format. The supplier cannot provide either. That is a red flag. The production capacity check fails because the supplier cannot prove the machines are tested before shipment. The supplier verification process weakens because the partner relationship is not documented. The sourcing decision changes. The manager may keep the supplier under review, but will not place a large order yet.
Common red flags on the factory floor
The factory floor is the first place where claims are tested. The auditor looks for evidence, not just verbal answers.
- Machines under construction are covered with dust or debris.
- Calibration tools are missing from workbenches.
- Operators cannot explain the current production step.
- Finished machines are stored outdoors without protection.
- There is no visible quality control station.
- Spare parts are mixed with raw materials.
- The assembly area is crowded and hard to move through.
Each of these points has a direct impact. If calibration tools are missing, the risk of out-of-tolerance machines rises. If operators cannot explain their task, the process may not be standardized. If finished machines are exposed to weather, corrosion and damage become likely.
A good auditor does not take these points at face value. The auditor asks for the quality control checklist. The auditor asks for the calibration log. The auditor asks for the storage policy. The answers either support the claim or expose the gap.
Supplier verification gaps to watch
Supplier verification is about confirming identity and capability. There are several areas where suppliers show weakness.
- The company name on the building differs from the contract entity.
- The sales team cannot introduce the factory manager or technical lead.
- The supplier cannot show a clear ownership chain for the machinery it sells.
- The supplier’s website lists machines that are not visible in the factory.
- The supplier cannot explain how it sources critical components.
- The supplier has no documented process for handling complaints.
- The supplier’s financial records are vague or unavailable.
These gaps do not always mean the supplier is dishonest. Sometimes the company is small and informal. Sometimes it is new to exporting. But they do mean the buyer has less certainty. The procurement manager must decide how much risk is acceptable.
A practical check is to ask for a sample purchase order, a delivery note, and a quality certificate from a past customer. The supplier should be able to provide these without long delays. If the documents are missing or inconsistent, the verification process is weak.
Production capacity check in practice
A production capacity check confirms that the supplier can build and deliver what it promises. It is not just a count of machines in the building. It includes labor, tooling, testing, and lead time.
The auditor should look at:
- The number of assembly bays and their size.
- The number of technicians working on spinning frames.
- The testing equipment available for speed, tension, and noise.
- The warehouse space for finished goods.
- The lead time for critical components.
- The backup plan if a supplier of a key part delays delivery.
A supplier with high demand may promise short lead times. But if the tooling is limited, the promise may fail. The production capacity check reveals this.
For example, a supplier may have one large assembly hall and three technicians. It may claim to deliver ten ring spinning frames in four months. The auditor asks for the schedule. The schedule shows that each frame needs two weeks for assembly and one week for testing. The math does not work. The red flag is clear. The production capacity is not enough for the promised volume.
The buyer then has options. The supplier may add shifts or subcontract. The buyer may reduce the order size. Or the buyer may look for another supplier. The decision depends on the project timeline and the risk tolerance.
How red flags affect sourcing decisions
Each red flag changes the sourcing decision in a specific way. The buyer must connect the warning sign to the commercial impact.
| Red flag | Sourcing impact |
|---|---|
| Missing calibration records | Higher risk of machine faults after installation |
| No documented partner for testing | Uncertainty over quality and delivery |
| Mixed spare parts storage | Slower response to breakdowns |
| Vague ownership chain | Risk of contract disputes and warranty issues |
| No quality control station | More rework and longer lead times |
| Unexplained component sourcing | Supply chain risk for future orders |
The buyer does not need to reject a supplier over one minor issue. But the issue must be addressed. If the supplier has no quality control station, the buyer may require a third-party inspection. If the spare parts storage is mixed, the buyer may require a separate warehouse. If the component sourcing is unclear, the buyer may require a list of approved suppliers.
The key is to make the risk visible. A red flag is not a reason to stop. It is a reason to add controls.
Building a reliable audit routine
A reliable audit routine uses the same checks every time. The procurement team creates a checklist based on past issues and industry standards. The checklist includes supplier verification, production capacity, spare parts availability, and technical support.
The auditor should bring a team. One person handles technical questions. One handles financial and legal checks. One handles logistics and delivery. The team works together during the visit.
After the visit, the team writes a report. The report lists the red flags, the evidence, and the supplier’s response. The report is shared with the buying committee. The committee decides whether to proceed, with conditions, or to stop.
The routine also includes follow-up visits. The supplier may improve after the first audit. A follow-up visit confirms the change. If the supplier does not improve, the risk remains.
A final note on communication. The auditor should be direct but professional. The goal is not to insult the supplier. The goal is to protect the buyer’s project. A clear conversation about a red flag is better than a vague comment that the supplier may ignore.
When to walk away
Some red flags are serious enough to end the evaluation. The buyer should consider walking away when the supplier cannot provide basic documentation, when the production capacity is clearly false, or when the quality process is absent.
A supplier that hides the factory floor is a warning. A supplier that refuses to show past customer references is a warning. A supplier that cannot explain how it tests its machines is a warning.
The buyer must weigh the cost of losing a supplier against the cost of a bad machine. A bad machine causes downtime, extra parts, and lost production. The audit exists to prevent that.
A worked example of walking away: a buyer visits a supplier for a compacting machine order. The supplier shows a small workshop. The machines are assembled by hand, with no testing equipment. The supplier says it uses a third party for testing but cannot name the third party. The production capacity check fails. The supplier verification is weak. The buyer decides not to proceed. The buyer keeps the supplier on a watch list but does not place an order. This decision protects the project and keeps the option open if the supplier improves.
The audit is not a one-time event. It is a tool for ongoing supplier management. The buyer who uses it well makes better decisions and faces fewer surprises.
Frequently asked questions
What is the most common factory audit red flag in spinning machinery?
Missing calibration and testing records are a frequent red flag. They suggest the supplier may not verify machine performance before delivery.
How does a production capacity check affect the supplier decision?
It reveals whether the supplier can actually build and ship the promised machines on time. If the capacity is too low, the buyer adjusts the order or seeks another supplier.
What documents should I request during a factory audit?
Request quality certificates, calibration logs, delivery notes, past purchase orders, and spare parts lists. These documents support supplier verification.
Can a small supplier still pass a factory audit?
Yes, if it has clear processes and can show evidence of quality and capacity. The size does not matter as much as the documentation and the floor conditions.
How often should I revisit a supplier after a red flag?
Revisit after the supplier makes the agreed changes. A follow-up visit confirms the fix and reduces risk before the next order.